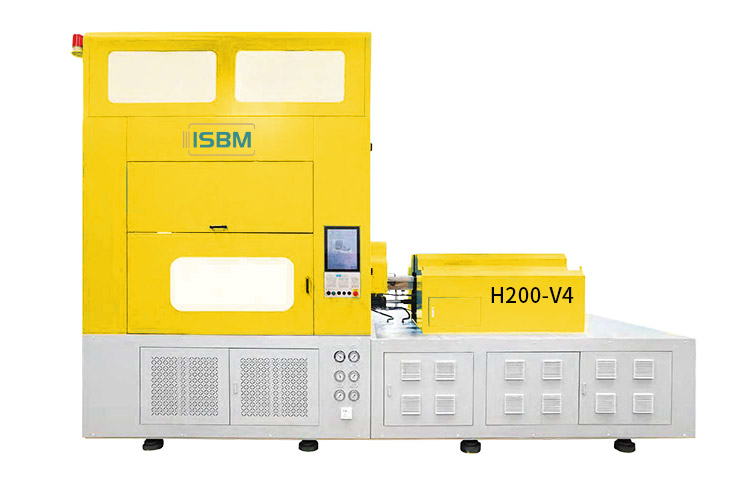
The H200-V4 provides a four-station PET/PETG configuration with product-quantity references extending to twelve PCS. Select it by matching the bottle geometry and tooling requirements to the specific reference row and mold proposal.
Review the bottle neck, available station movements and selected injection option for your project.
The listed quantity entries are 1 ~ 8, 10 and 12 PCS. Confirm how each relates to the actual mold and active cavities. Installed power is an electrical rating, not measured operating consumption.
Model overview
Review the Mold Space and Bottle Neck
The H200-V4 lists injection upper and lower strokes of 460 mm and 210 mm. Check these movements against the complete tool opening, neck support and removal sequence, alongside the proposed bottle dimensions.
The one-piece product reference includes a 118 mm body and 83 mm neck. The three-piece entry lists a 105 mm body and 68 mm neck. Both have a 210 mm height reference, but each row describes its own matched container arrangement.
Select the relevant product row before discussing output. The mold proposal should identify the active cavities, bottle quality requirements and cycle conditions used to establish accepted production.
Form the preform with the selected screw, resin grade and proposed injection tool.
02
Conditioning
Prepare the preform for stretch blowing within the conditioning tool and available movements.
03
Stretch Blowing
Stretch and blow the preform to the approved bottle geometry and neck-handling arrangement.
04
Take-Out
Remove the molded container using the planned clearance and take-out sequence.
Technical data
H200-V4 Machine Specifications
Identify the selected screw option with the PET or PETG grade and target bottle mass. Review each station movement against the proposed tooling sequence.
Machine
Parameter
Specification
Drive
Hydraulic
Stations
4
Specified materials
PET, PETG
Dimensions, L × W × H
4.8 × 2.0 × 3.2 m
Machine weight
13 t
Oil tank capacity
300 L
Electrical, Air and Cooling
Parameter
Specification
Motor power
49.2 kW
Heating power
10 kW
Total installed power
59.2 kW
Blowing-air pressure
2.0 ~ 3.5 MPa
Cooling-water pressure
0.4 ~ 0.6 MPa
Oil-cooler water pressure
0.3 ~ 0.4 MPa
Oil-cooler water temperature
20 ~ 25 °C
Voltage
370 ~ 400 V
Injection Screw Options
Screw diameter
Theoretical injection volume
Rotation speed
40 mm
240 cm³
270 rpm
50 mm
350 cm³
220 rpm
55 mm
450 cm³
220 rpm
60 mm
600 cm³
220 rpm
Keep each screw diameter, theoretical volume and rotation speed paired. Confirm usable shot mass for the selected resin and preform; theoretical volume is not a bottle-weight rating.
Station and Mold Movements
Parameter
Specification
Injection clamping force
300 kN
Injection upper stroke
460 mm
Injection lower stroke
210 mm
Conditioning core stroke
250 mm
Conditioning cavity stroke
250 mm
Blow clamping force, single side
200 kN
Blow core stroke
300 mm
Blow mold stroke
75 + 75 mm
Take-out stroke
175 mm
Assess mold space through the full station sequence. Injection opening, conditioning movements, blow-core travel and container removal address different tooling needs. Review the complete tool and neck-support arrangement rather than bottle height alone.
Container configuration
Product References: 1 ~ 8, 10 and 12 PCS
The first four entries have a 210 mm height reference, with body diameters of 118, 110, 105 and 100 mm. Later entries pair smaller bodies with 150 or 100 mm heights.
Swipe horizontally to view all columns.
QuantityPCS
Body diametermm
Bottle heightmm
Neck sizemm
Weight referenceg
1
118
210
83
150
2
110
210
68
65
3
105
210
68
45
4
100
210
65
35
5
68
150
55
30
6
65
150
50
28
7
48
150
40
25
8
45
150
25
20
10
38
100
23
15
12
26
100
15
10
Read each row as one matched reference. Body, neck, height and weight limits from different rows must not be combined. Final suitability depends on the bottle, preform and mold design.
PCS retains the catalog's product-quantity label. Confirm the actual cavity arrangement and accepted containers per cycle before calculating output. These rows do not establish a cycle time.
Drive and component configuration
Define the Supplied Control and Actuation Package
Review the servo-pump combination, control equipment and actuation options with the selected screw and mold. The quotation should identify the actual supplied package and any substitutions.
Drive and Control Systems
Item
Catalog reference
Servo-pump package
Inovance with Sumitomo or WEICHI with OFITE
PLC
Inovance or MIRLE
Blow-clamp actuation
Hydraulic or dual-servo option
Plasticizing drive
Hydraulic or servo option
Valves and Temperature Control
Item
Catalog reference
High-pressure valve
Parker
Air cylinder
AirTAC
Hydraulic valve
YUKEN
Temperature control
Integrated control box or built-in system
The listed brands and alternatives describe the catalog reference. They do not mean that every alternative is included in one machine.
Tooling and installation
Match the Tooling Sequence to the Plant Layout
Connect the bottle and neck drawings with the tool opening, support and removal requirements. Prepare the utility and floor-space schedule for the selected H200-V4 configuration.
Use the Injection Strokes to Review the Tool
The 460 mm upper and 210 mm lower injection strokes are the starting references for the standard H200-V4 proposal. Review them against the actual injection tool, neck components and opening sequence.
Conditioning core and cavity strokes are both 250 mm. The blow-core stroke is 300 mm and the take-out stroke is 175 mm. Check the space required at each station, including the removal path for the finished container.
If the bottle or tooling requires a different height, neck or stroke envelope, compare the H200-V4B as a separate configuration.
Plan the Machine Services and Access
The listed envelope is 4.8 × 2.0 × 3.2 m, with a weight of 13 t. Confirm service access, mold handling and auxiliary-equipment positions in the proposed production-cell drawing.
The 49.2 kW motor entry and 10 kW heating entry give a total installed power of 59.2 kW. Show auxiliaries separately from the molding-machine rating in the electrical schedule.
Confirm cooling and blowing-air capacity at the machine connection. Keep the machine cooling-water and oil-cooler circuits separate, and provide access to the 300 L oil tank.
Length
4.8 m
Width
2.0 m
Height
3.2 m
Related configuration
Know When to Compare H200-V4B
The H200-V4B has different injection strokes and a different neck and height reference. Review it when the bottle or tooling requirements call for that alternative envelope.
A larger clearance or neck entry does not automatically improve output or make the B configuration necessary for every container. Compare the full tool and installation proposal using the same bottle drawing.
Clarify the alternative mold-space configuration, paired screw values and output assumptions before final selection.
When is H200-V4B worth comparing?
When the bottle or tooling review requires its different height, neck or stroke envelope. A bottle that fits H200-V4 does not automatically benefit from selecting the B configuration.
Do all screw options run at the same speed?
No. The 40 mm column lists 270 rpm, while the 50, 55 and 60 mm columns list 220 rpm. Keep those option values paired.
Does the table establish the cycle time?
No cycle time is provided for a defined bottle. Establish it through the mold proposal and trial, then calculate output using active cavities and accepted quality.
Discuss your bottle and mold
Prepare an H200-V4 Proposal
Provide the bottle and neck drawings, resin grade, target mass, required accepted output and existing mold details. Request the selected screw, mold layout, utility schedule and bottle acceptance criteria in the proposal.
Body, height and neck-finish drawing
PET or PETG grade and target bottle mass
Preform, mold interfaces and existing-tool details
Required accepted output and trial criteria
Available floor space and utility connections
Share a drawing link in the message, or send your files to info@isbmmachine.net.
Include any tooling constraints that may require comparison with H200-V4B.