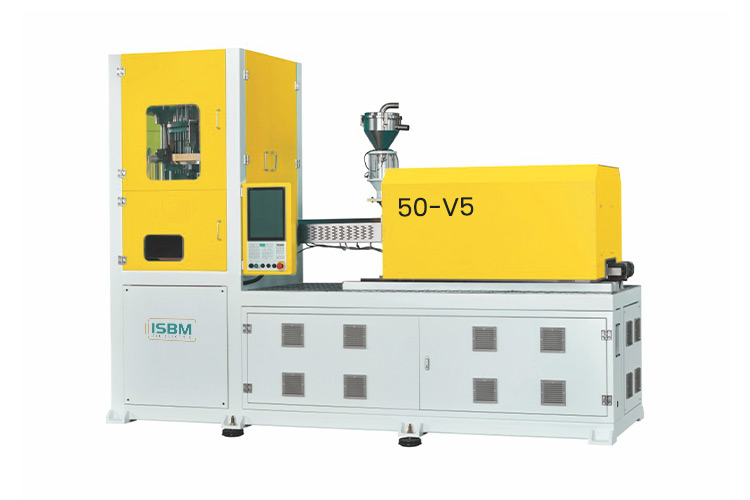
The 50-V5 integrates preform injection, stretch blowing and take-out in a three-station machine. Its selection table covers one to six cavities, with a different bottle envelope for each arrangement.
Evaluate the actual cavity row against your container drawing before choosing the mold configuration.
The one-cavity reference lists a maximum body diameter of 90 mm and a 60 mm neck. At six cavities, the corresponding reference is a 28 mm body diameter and a 17 mm neck. The listed maximum bottle height is 200 mm.
These are configuration-dependent limits. Each cavity arrangement needs its own bottle and mold assessment.
Form the preform for the selected bottle and mold arrangement.
02
Stretch Blowing
Stretch and blow the preform into the container.
03
Take-out
Remove the container through the configured take-out sequence.
Technical data
50-V5 Machine Specifications
Review the injection unit, station movements and machine envelope together when defining the proposed mold and production configuration.
Machine
Parameter
Specification
Stations
3
Installed power
20 kW
Dimensions, L × W × H
3.4 × 1.2 × 2.5 m
Machine weight
3.5 t
Injection Unit
Parameter
Specification
Screw diameter
35 mm
Theoretical injection volume
130 cm³
Injection rate
90 cm³/s
Injection pressure
160 MPa
Screw rotation speed
0–200 rpm
Station and Mold Movements
Parameter
Specification
Injection clamping force
100 kN
Injection upper stroke
450 mm
Injection lower stroke
225 mm
Blow clamping force
70 kN
Blow core stroke
200 mm
Blow mold opening stroke
70 mm
Take-out stroke
100 mm
Installed power is used for electrical planning. Operating consumption must be measured for the agreed bottle, mold and auxiliary equipment.
Evaluate the proposed mold with the injection specification. The 35 mm screw, 130 cm³ theoretical injection volume, 90 cm³/s injection rate and 160 MPa injection pressure describe the injection unit. The tool proposal should connect bottle weight to the total shot requirement and identify the cycle used to calculate finished-bottle output.
Bottle configuration
One to Six Cavities, with Matched Bottle Limits
Read each row as one configuration reference. Body diameter, neck size, height and weight from different rows must not be combined.
Swipe horizontally to view all columns.
Cavities
Body diametermm
Bottle heightmm
Neck sizemm
Bottle weightg
1
90
200
60
105
2
80
200
38
50
3
64
200
30
35
4
45
200
27
28
5
35
200
20
22
6
28
200
17
18
Catalog configuration references. Final suitability depends on the complete bottle, preform and mold design. The six-cavity reference applies to a smaller container than the one-cavity reference.
Project planning
Check Tooling Clearance and Installation Space
Use the machine dimensions and movement data to review the complete working cell, including tool access and container removal.
A Defined Starting Point for Compact Layouts
The 50-V5 combines a 3.4 m machine length with a 1.2 m width and a 2.5 m height. These dimensions help your production team begin its layout study alongside material preparation, cooling equipment and container handling.
The machine envelope is only part of the working cell. Allow access to the mold, injection unit and service connections, including the path used to remove a mold.
Length
3.4 m
Width
1.2 m
Height
2.5 m
Match Clearance as Well as Bottle Dimensions
The injection station lists 450 mm of upper stroke and 225 mm of lower stroke. The blow station lists a 200 mm core stroke and a 70 mm mold opening stroke, followed by a 100 mm take-out stroke.
These dimensions describe different machine movements. Check preform tooling, neck handling and the removal sequence against the machine interface drawing, even when the finished bottle fits a listed size row.
Related model
Compare the Injection Unit with the 50-S6
A similar bottle-size table does not establish identical injection capability or operating costs. The two models have different injection-unit specifications and strokes, so the tooling needs a separate review.
Clarify the cavity references, electrical rating and comparison points before requesting a machine configuration.
Does the six-cavity entry apply to the largest bottle?
No. The six-cavity row lists a 28 mm body and a 17 mm neck, while the one-cavity row lists 90 mm and 60 mm. Each row describes a different configuration.
Is the 20 kW figure the running electricity consumption?
It is the catalog installed-power figure. Operating consumption needs a measurement for the agreed bottle, mold and auxiliaries; it cannot be calculated from that figure alone.
What distinguishes this model from the 50-S6?
The catalog injection units differ: 50-V5 lists a 35 mm screw and 130 cm³ theoretical injection volume, whereas 50-S6 lists 36 mm and 146 cm³. Their injection strokes also differ, so tooling needs separate review.
Discuss your bottle project
Request a 50-V5 Configuration
Send your bottle requirements for a quotation covering the injection unit, mold cavitation, utility requirements and included auxiliary equipment.
Bottle drawing and neck finish
Resin grade and target bottle weight
Required accepted bottles per hour
Existing mold information, if applicable
Available space and local power supply
Include a drawing link in your message, or email your drawing to info@isbmmachine.net.
Cycle time and accepted output should be established using the proposed bottle and mold.